Jack Pad Mount Repair
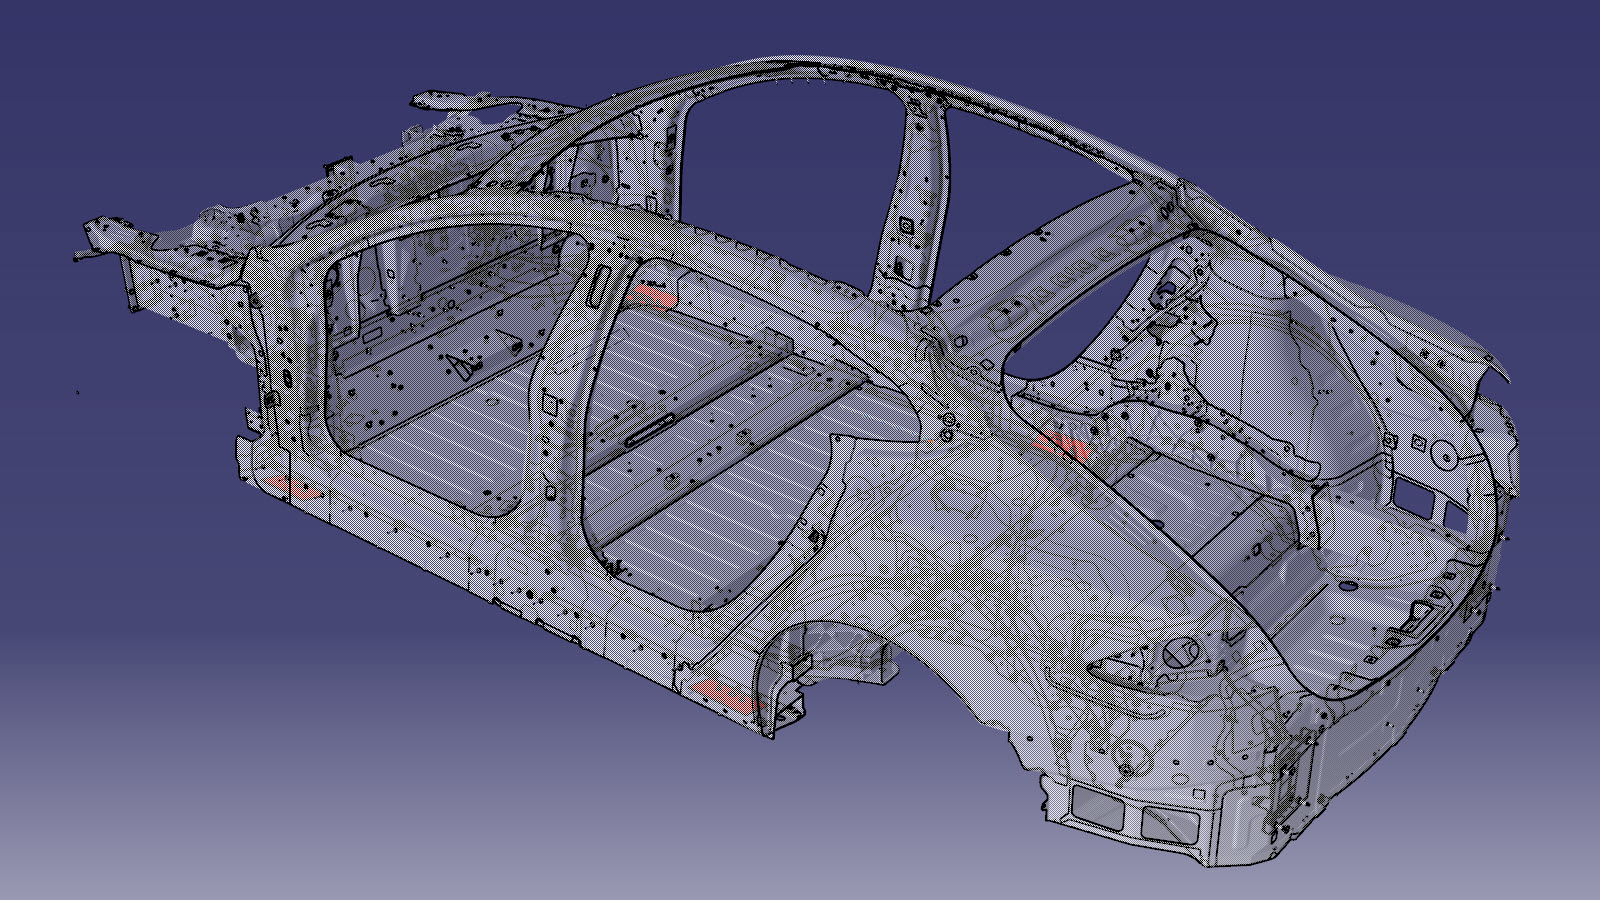 Correction code:
10102904002
NOTE:
Unless explicitly stated in the procedure, the above
correction code includes all Collision Repair and Service
repair work required to perform this procedure, including
the linked Collision Repair procedures and linked Service
procedures. Do not stack Collision Repair correction
codes unless explicitly told to do so. Depending
on the damage to the vehicle, additional repairs may be
required.
Repair Information
- Review all collision repair general practices and safety documentation and wear the appropriate PPE (Personal Protective Equipment) before beginning this procedure.
- This procedure can be completed without using a frame bench.
Parts List
| Quantity | Description | Image / Notes |
|---|---|---|
| 1 | PLATE- SERVICE SIDE SILL (Jack Pad Mount Repair Plate) | |
| 9 | ||
| 2 |
Rivnut, M8x0.5-3 |
Tesla part number 1014282-00-A. |
When ordering parts, refer to the Parts Catalog and enter the VIN of the vehicle being repaired to find the correct parts (and the part numbers) for the vehicle. Alternatively, use the search function in the Parts Catalog to find a specific part for the vehicle.
Repair Procedure
- Remove the Molding - Rocker Panel - LH (Remove and Replace).
- Remove the HV Battery (RWD/AWD) (Remove and Install).
-
Remove the original component.
Rivnut
- Repair any bends in the Pick Up Hole area.
-
If there are cracks 10 mm or
longer in the repair area, perform GMA welding.
WarningFailure to follow all welding safety precautions, including the use of personal protective equipment, could result in serious injury or property damage. Only technicians who have completed Tesla’s approved welding training are authorized to weld structural components on Tesla vehicles.WarningTo maintain vehicle crash integrity, use only approved welding wire and an approved GMA welder to perform GMA welding on Tesla vehicles. Refer to Approved Gas Metal Arc (GMA) Welders and Welding Wire for information on approved GMA welders and welding wire.CAUTIONDo not weld on a Tesla vehicle before performing the Vehicle Electrical Isolation Procedure (refer to the vehicle-specific Service Manual for more information on the Vehicle Electrical Isolation Procedure). Welding on a Tesla vehicle with an energized high or low voltage system might damage vehicle components.NoteBefore GMA welding, a test weld using material of the same gauge and type should be performed to make sure that the welding equipment settings produce a satisfactory joint.
- If necessary, grind the top surface of welds to make the weld flush with the surrounding area.
-
Position the repair plate and mark the outline of the Pick Up hole (center)
and the Rivnut holes.
- Drill a 16 mm hole for a Rivnut in each of the marked locations.
- Drill a 25 mm hole in the location marked for the Pick Up hole.
-
Prepare for installation.
or Structural Countersunk Rivets, 6.5 mmNoteMark holes for countersunk rivets approximately 35 mm apart, and at least 18 mm away from the corners, edges, holes, or obstructions to provide enough clearance for the Microstop countersink cage assembly. In areas where more than one row of countersunk structural rivets will be installed, offset each row of rivets from the row above and below (as shown).
Rivnut
- Apply structural adhesive to the mating surfaces on the vehicle and the new component or components.
- Install the new component or components.
- Perform any necessary post-repair operations.
- Install the HV Battery (RWD/AWD) (Remove and Install).
- Install the Molding - Rocker Panel - LH (Remove and Replace).